Engro Fertilizers
Chemical and Process Engineering Intern · Summer 2016 · Daharki, Sindh, Pakistan
At Engro Fertilizers, I studied the ammonia synthesis loop. I used Aspen HYSYS, a process simulation program, and the plant's own operating data. I also worked on cooling-tower performance and equipment warranty claims. The internship taught me a habit I still use. Compare the model with what the plant is really doing. Then use the gaps to make an operating decision.
Cooling-tower system
Measured after the changes were made.
Equipment warranty claims
Capital and operating savings. The claims also helped restore production capacity.
The ammonia loop
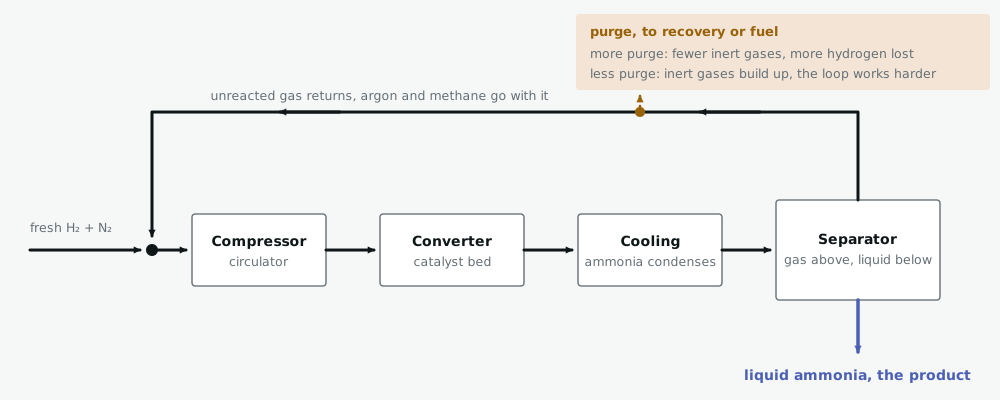
Hydrogen and nitrogen do not all react in one pass. The gas that did not react goes back around the loop. Argon and methane do not react at all, so they build up. A purge removes them. But the purge also takes some hydrogen with it. I led an Aspen HYSYS analysis of the loop, using the plant's operating data. The work helped find equipment faults and put a cost on each one. That gave the operations team a clearer basis for troubleshooting.
- Fresh hydrogen and nitrogen join recycled gas.
- The gas goes through the compressor and then the converter, where ammonia forms.
- Cooling turns the ammonia into a liquid. The separator sends the liquid out as the product.
- The gas that is left goes back around the loop. A small purge removes the argon and methane that build up.
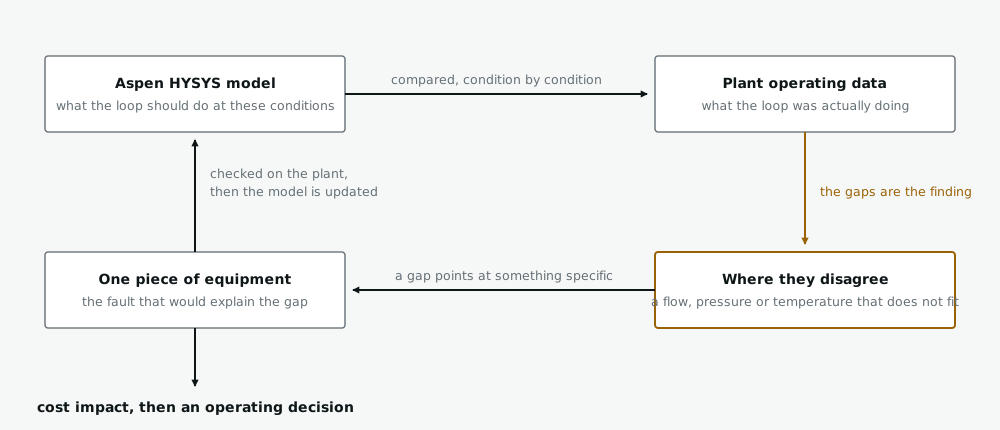
- The Aspen HYSYS model says what the loop should be doing at the plant's conditions.
- The plant's operating data says what the loop was really doing.
- Where the two disagree, one reading does not fit: a flow, a pressure or a temperature. That gap points at one piece of equipment.
- The idea is checked on the plant. Then the model is updated.
The cooling towers
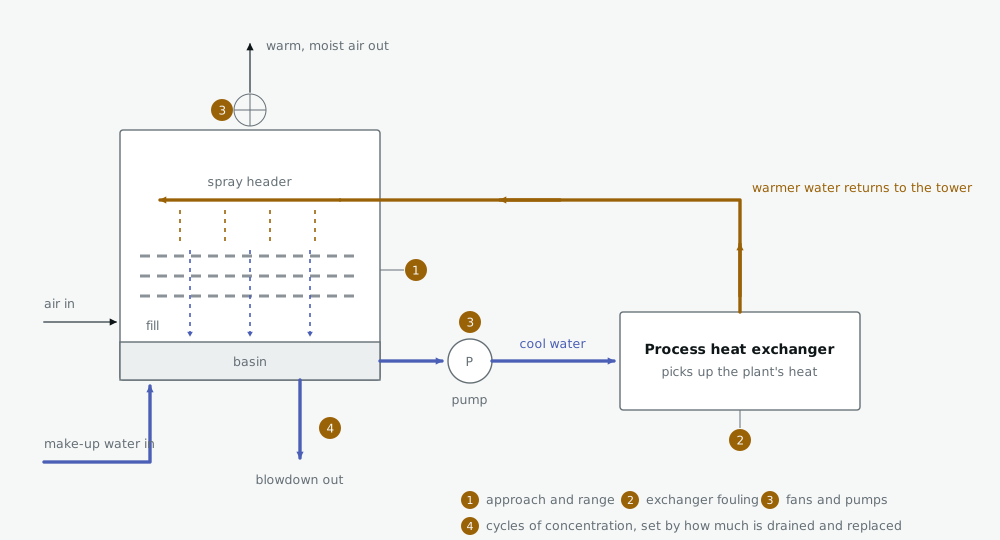
I reviewed four things in the cooling-tower system: approach and range, fouling in the heat exchangers, the fans and pumps, and cycles of concentration. Approach and range mean how much the water cools in the tower, and how close it gets to the lowest temperature the air can give. Fouling is scale and dirt on the heat-exchanger surfaces. Cycles of concentration is set by how much water is drained and replaced. It decides how concentrated the minerals get. Changes from this work cut energy use in the cooling-tower system by 7% and water use by 18%. Both numbers were measured after the changes were made.
- Cool water leaves the basin at the bottom of the tower. A pump moves it on.
- In the heat exchanger, the water picks up heat from the plant.
- The warm water goes back to the top of the tower. It falls through the fill and cools as some of it evaporates.
Warranty recovery
I also negotiated equipment warranty claims. The claims secured $0.4M+ in capital and operating savings combined. They also helped restore production capacity.
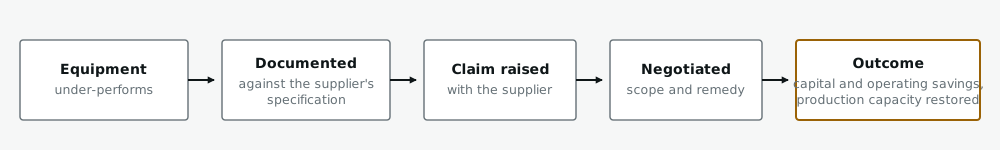
- A piece of equipment does not perform as it should.
- Its real performance is written up next to what the supplier promised in the specification.
- A claim is raised with the supplier.
- The two sides negotiate what the claim covers and how the supplier will put it right.
- Outcome: capital and operating savings, and production capacity restored.
What I learned
At Engro, a model was useful when it helped the team find one specific problem and check whether a fix worked. I kept that habit. It later shaped how I worked on membrane products and data-center cooling.